A practical guide to metal foam manufacturing for engineers, product developers and material buyers
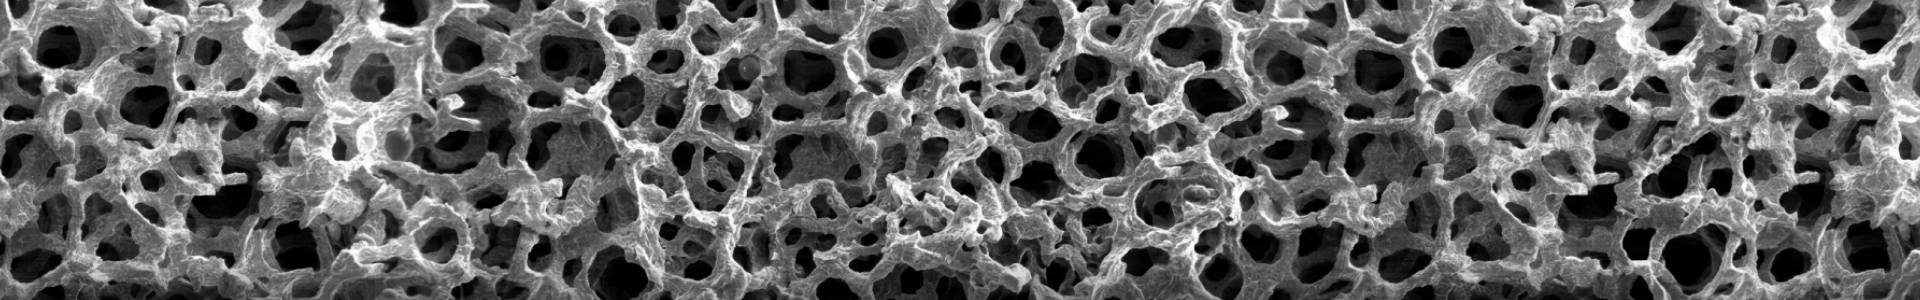
Metal foam is made by creating and stabilizing thousands of pores inside a solid metal matrix — either by injecting or releasing gas into molten metal, foaming a compacted metal-powder precursor, depositing metal onto a foam template, or removing a sacrificial pore-former from a sintered body. Which metal foam production process a manufacturer chooses depends on the required pore structure (open-cell or closed-cell), the base metal, target porosity, density and end application. This guide walks through the main manufacturing routes step by step and explains how each one shapes the properties of the final material.
If you are new to the material itself, start with our overview of what metal foam is and its core characteristics — this article focuses specifically on how it is manufactured.
How Is Metal Foam Made? The Basic Manufacturing Sequence
Regardless of the specific route, most metal foam manufacturing follows the same logic: create pores, keep them from collapsing, and lock the structure into a solid. The typical sequence looks like this:
- 1. Metal preparation — the base material is melted, milled into powder, or prepared as a slurry or solution, depending on the process.
- 2. Pore creation — gas is injected or chemically released into the melt, a blowing agent decomposes inside a powder compact, or a sacrificial template defines where the pores will be.
- 3. Pore stabilization — viscosity modifiers, stabilizing particles, compaction pressure or sintering necks prevent the pores from merging or collapsing while the metal is still soft.
- 4. Solidification or deposition — the foamed melt cools, the powder compact sinters, or metal is electrodeposited and the template is burned out.
- 5. Cutting and finishing — the foam block, panel or sheet is sliced, rolled, machined or formed into the required thickness and dimensions.
- 6. Quality inspection — porosity, pore size or PPI, density, thickness and mechanical or electrical properties are measured against specification.
The details differ significantly between methods — and those differences explain why two metal foams with similar porosity can behave very differently in service.
Main Metal Foam Manufacturing Methods
There are four established metal foam production methods used across the industry today. Each produces a characteristic pore structure and suits different materials and applications.
1. Melt Foaming
Principle: gas is introduced directly into molten metal, and the resulting bubble structure is stabilized and frozen in place as the melt solidifies. This is the standard route for closed-cell aluminum foam and is well documented in cellular metals literature (for example, Banhart's Manufacture, Characterisation and Application of Cellular Metals and Metal Foams, 2001).
Process steps: melt the metal (usually aluminum or an aluminum alloy) → raise melt viscosity by adding stabilizing particles (such as SiC or Al₂O₃) or calcium → introduce gas either by bubbling air or nitrogen through a rotating impeller, or by adding a blowing agent such as titanium hydride (TiH₂), which decomposes and releases hydrogen → hold the foaming melt in a mold for a controlled time → cool and solidify → cut the foam block into panels or parts.
Typical pore structure: closed, discrete cells roughly 1–5 mm in size; porosity commonly in the range of 80–95%.
Typical applications: crash and impact absorbers, lightweight structural panels, aluminum foam sandwich cores, sound insulation in combination with perforated facings.
Advantages and limitations: melt foaming can produce large panels at relatively low material cost, but it is mostly suited to aluminum, and controlling cell size distribution across a large block is challenging.
2. Powder Metallurgy
Principle: a dense "precursor" is made from metal powder mixed with a small amount of blowing agent. When the precursor is heated above the alloy's solidus temperature, the blowing agent releases gas and the compact foams in place — a key advantage is that foaming happens inside a mold or between face sheets, so shape is fully controlled.
Process steps: mix metal powders with a foaming agent (TiH₂ is the classic choice for aluminum) → compact, extrude or roll the mixture into a dense precursor → place the precursor in a mold, a cavity, or between two metal face sheets → heat above the foaming temperature so the material expands → cool under controlled conditions → finish.
Typical pore structure: predominantly closed cells with relatively fine, fairly uniform porosity; cell geometry can be tuned through precursor composition and heating profile.
Typical applications: aluminum foam sandwich (AFS) panels, near-net-shape foam parts, foam-filled hollow profiles and energy-absorbing structures.
Advantages and limitations: powder metallurgy offers excellent shape freedom and works with many alloys, and it is the natural route for sandwich manufacturing because the core and skins are bonded during foaming. On the other hand, precursor material is more expensive than molten metal, and production is typically batch-based.
3. Electrodeposition and Replication
Principle: instead of foaming the metal itself, this metal foam fabrication route copies an existing porous template. In electrodeposition, an open-cell polymer foam is made electrically conductive, plated with metal in an electroplating bath, then heated to burn out the template and sinter the metal — leaving a pure metal replica of the original foam. In replication, molten metal or a metal slurry is infiltrated into a removable preform (such as a bed of salt particles), which is later dissolved or washed out.
Process steps (electrodeposition): prepare open-cell polyurethane foam template → apply conductive coating (graphite or electroless plating) → electroplate nickel, copper or another platable metal to the target thickness → thermally remove the polymer template → sinter and reduce → cut to thickness.
Typical pore structure: fully open, interconnected cells replicating the template; very high porosity, commonly above 90–95%; available in a range of PPI (pores per inch) grades.
Typical applications: nickel foam battery electrodes and current collectors, catalyst and catalyst-carrier substrates, heat exchangers, filters, silencers, EMI shielding.
Advantages and limitations: electrodeposition gives the highest porosity and the most controllable PPI of any common method, which is why most commercial nickel foam is made this way. Limitations include restricted material choice (the metal must be platable or infiltratable) and practical limits on achievable thickness.
4. Space-Holder and Casting Methods
Principle: pores are defined by a sacrificial "space holder" mixed into the metal before sintering, or by casting metal around a removable pattern. Because the holder determines pore size and shape directly, this route offers some of the tightest pore control in metal foam production.
Process steps (space-holder): mix metal powder with spherical or granular spacer particles (sodium chloride, urea or polymer spheres) → compact the mixture → remove the spacer by water leaching or thermal burnout → sinter the skeleton into a continuous metal structure → finish.
Typical pore structure: open, interconnected pores whose size and shape mirror the space-holder particles; porosity typically adjustable over a wide range.
Typical applications: titanium foam implants with bone-ingrowth porosity, high-precision filters and flow restrictors, customized porous components.
Advantages and limitations: precise pore geometry and compatibility with high-value metals such as titanium; but spacer removal adds process steps, and very high porosities are harder to reach than with template methods.
Open-Cell vs Closed-Cell Metal Foam Manufacturing
The single most important question when asking how metal foam is made is: are the pores connected or sealed? That one difference determines which manufacturing route is possible — and what the foam can be used for.
| Feature | Open-Cell Metal Foam | Closed-Cell Metal Foam |
|---|---|---|
| Pore structure | Interconnected pore network; gases and liquids flow through the material | Sealed, discrete cells; pores isolated from one another |
| Typical manufacturing methods | Electrodeposition on foam template, space-holder plus sintering, replication/investment casting | Melt foaming (gas injection or blowing agent), powder metallurgy foaming |
| Fluid permeability | High — fluids pass straight through | Very low — cells are sealed |
| Specific surface area | Very high (porosity typically above 90%) | Lower relative to open-cell foam |
| Typical applications | Battery electrodes, catalyst supports, filtration, heat exchangers, silencers, EMI shielding | Crash absorbers, lightweight sandwich panels, sound insulation, structural stiffening |
| Key manufacturing parameters | PPI / pore size, porosity, thickness, metal type, plating or sintering conditions | Blowing agent content, melt viscosity, holding time, cooling rate, foam density |
In short: closed-cell processes make foams that block fluids and absorb energy, while open-cell processes make foams that let fluids pass and expose maximum metal surface area. Matching the structure to the function is the core of metal foam material selection.
What Controls Metal Foam Properties?
Beyond the manufacturing route, several specification-level parameters determine how a metal foam performs:
- Porosity — the fraction of the volume that is pore space. Higher porosity means lower weight and larger surface area, but lower strength and stiffness.
- Pore size — smaller pores raise capillary and filtration precision and increase pressure drop; larger pores flow more freely.
- PPI (pores per inch) — the standard grading for open-cell foam. Higher PPI means finer pores and greater specific surface area, which matters for electrodes, catalyst supports and heat transfer.
- Density — mechanical strength of metal foam scales strongly with relative density, making it a critical input for structural and energy-absorbing designs.
- Thickness — affects pressure drop, current distribution, thermal path length and mechanical behavior, especially in electrodes and heat exchangers.
- Metal or alloy — electrical and thermal conductivity, corrosion resistance, temperature capability and cost are all set by the base material choice.
How Manufacturing Methods Affect Different Metal Foam Products
Each commercial metal foam material exists because a particular production process can deliver the pore structure that application needs. Here is how the main material families map to their typical manufacturing routes.
Nickel Foam is the classic electrodeposition product: an open-cell template replicated in pure nickel, delivering porosity above 90% in a range of PPI grades. That combination — high surface area, good conductivity, controllable pore size — is exactly why nickel foam dominates battery electrodes, catalyst substrates and electrolysis applications.
Copper Foam is likewise produced by deposition or sintering routes and is chosen primarily for thermal and electrical performance. Copper foam serves as heat-exchange and heat-sink media, battery current collectors and filter structures where both conductivity and flow are required.
Silver Foam combines high electrical conductivity with antibacterial and catalytic behavior, and is typically produced by deposition or sintering techniques for specialized electrochemical and functional applications.
Nickel-Chromium Foam and Nickel-Chromium-Aluminum Foam are engineered for elevated-temperature service. These alloy foams are generally produced by powder-based sintering routes, which allow the alloy composition to be built into the skeleton itself, making them suitable for burner media, catalyst carriers and high-temperature filtration.
Copper-Nickel Foam layers corrosion resistance on top of copper's thermal conductivity, produced through sintering or composite deposition — a common choice for heat exchange and electrochemical equipment exposed to aggressive media.
Carbon Foam and Silicon Carbide Foam extend the same template-replication concept beyond metals: a polymer foam template is coated or infiltrated, then carbonized or reaction-bonded into SiC. The result is a reticulated porous structure for high-temperature filtration, catalyst supports and burner applications where metals would not survive.
You can compare all of these options on our metal foam materials overview page.
HY Metal Foam / Huayan Intelligent Technology Co., Ltd. provides porous metal materials and customized metal foam solutions. According to the company's public product information, its capabilities include sintering and deposition techniques, with customization of pore structure, PPI, density, dimensions and other specifications. Because different products rely on different manufacturing routes, buyers should confirm the production process and specification options for each material directly with the supplier.
FAQ About Metal Foam Manufacturing
1. How is metal foam made?
Metal foam is made by creating and stabilizing pores in a metal matrix. The main routes are melt foaming (gas into molten metal), powder metallurgy (a blowing agent expands a powder compact), electrodeposition onto a foam template, and space-holder or replication methods where a sacrificial material defines the pores and is then removed.
2. How is open-cell metal foam made?
Open-cell metal foam is typically made by copying a template: an open-cell polymer foam is electroplated with metal and then burned out, or metal is cast or sintered around a removable space-holder that is later dissolved. The result is a fully interconnected pore network with high porosity, graded by PPI.
3. How is closed-cell metal foam made?
Closed-cell metal foam is made by introducing gas into molten metal — either by injecting gas through the melt or by adding a blowing agent such as TiH₂ — while stabilizing particles keep the bubbles from collapsing. Powder metallurgy foaming of a compacted precursor is the other main closed-cell route, and both are mostly used for aluminum foam.
4. What metals are commonly used to make metal foam?
Aluminum is the most widely used metal for closed-cell structural foam. Nickel and copper dominate open-cell electrodeposited foams for energy and thermal applications. Other options include titanium foam for medical implants, silver foam, and alloy foams such as nickel-chromium, nickel-chromium-aluminum and copper-nickel, plus carbon and silicon carbide foams for extreme temperatures.
5. Can metal foam be customized?
Yes. Depending on the manufacturing method, suppliers can customize pore size or PPI, porosity and density, thickness, sheet dimensions and material composition. For custom requirements, it is best to specify the application conditions so the supplier can recommend the right material and pore structure.
From Manufacturing Process to the Right Product
Understanding how metal foam is made makes material selection much easier: melt foaming and powder metallurgy deliver closed-cell structures for energy absorption and lightweight panels, while template deposition and space-holder routes deliver the open-cell networks that batteries, catalysts, filters and heat exchangers depend on.
If your project needs nickel foam, copper foam, alloy foam or other porous metal materials with a specific pore structure, density, PPI and dimensions, you can discuss your application requirements directly with HY Metal Foam — the team can help match the right material and specification to your use case.